A plated through hole is drilled through the entire board, but a high-speed signal usually uses only part of it. The unused copper below the signal layer is a stub, and at multi-gigabit rates it behaves like a resonant transmission line hanging off the trace.
Backdrilling removes that stub with a controlled-depth drill after plating. It is one of the few process steps that improves signal integrity without changing the layout, and one of the easiest to get wrong on depth.
This article covers what the stub does, how backdrilling works, where the cost comes from, and what to put on the fabrication drawing.
What a stub does
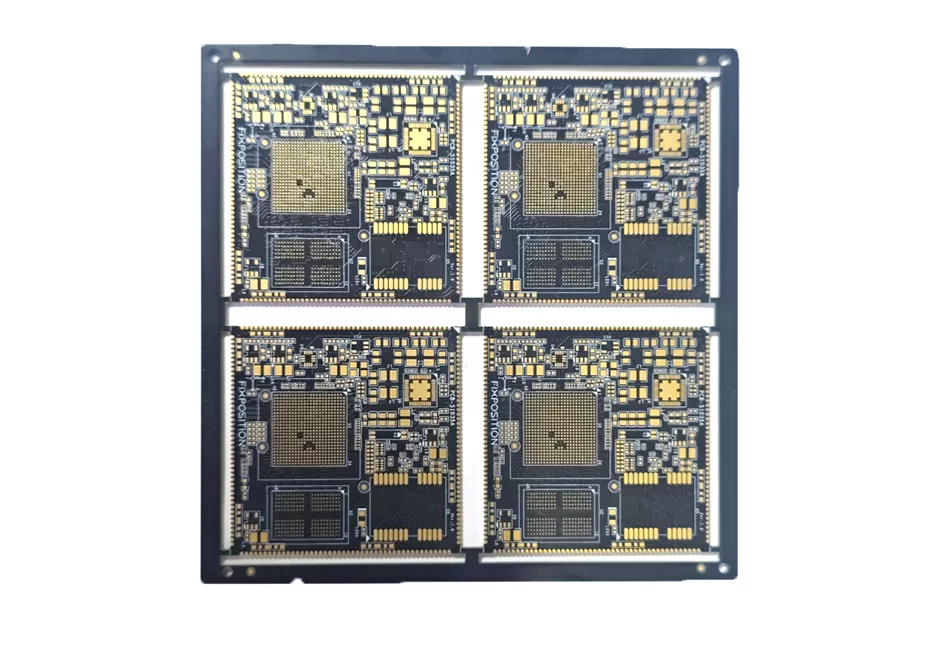
A via stub is the unused portion of the barrel below the layer where the signal enters or leaves. At low frequency it is invisible. As the data rate rises, the stub becomes a quarter-wave resonator: it reflects energy at a frequency set by its length and the dielectric.
The symptoms are familiar:
- Insertion loss peaks at specific frequencies.
- Return loss degrades at the same frequencies.
- Eye height and width shrink at the receiver.
- The effect gets worse as the stub gets longer, not as the trace gets longer.
The fix is either a different layer stackup, a blind/buried via, or backdrilling. Backdrilling is usually the cheapest of the three for a through-hole design.
How backdrilling works
After plating and before solder mask, the board is drilled from the opposite side with a bit slightly larger than the via. The drill stops at a controlled depth, removing the unused barrel while leaving the connection at the target layer intact.
The process has four critical variables:
- Depth control. The drill must stop above the target layer without cutting into the barrel that carries the signal.
- Drill diameter. Too small and it cannot remove the stub; too large and it eats the annular ring or the antipad.
- Registration. The backdrill must be concentric with the original via, or it will thin the barrel on one side.
- Residue. Drilling leaves debris; the hole must be cleaned before the next process.
A small stub always remains below the target layer. The goal is to make it short enough that its resonance is above the signal bandwidth, not to remove it completely.
Where the cost comes from
Backdrilling is a second drilling operation with its own setup, depth control and inspection. The cost drivers are:
- Number of backdrilled vias per panel.
- Depth tolerance required: tighter depth means slower drilling and more scrap.
- Via diameter and aspect ratio: small, deep vias are harder to backdrill cleanly.
- Registration capability of the drill.
- Inspection: cross-sections and, in some cases, X-ray.
- Yield loss from depth errors and annular ring damage.
The step is usually quoted per panel or per via, and it scales with the number of layers the signal has to pass through.
DFM rules
| Parameter | Typical requirement | Why it matters |
|---|---|---|
| Target stub length | 0.2–0.3 mm | Keeps resonance above the signal band |
| Backdrill diameter | Via + 0.2–0.3 mm | Removes the barrel without cutting the pad |
| Depth tolerance | Per fabricator capability | Too deep cuts the signal layer |
| Registration | Concentric with the via | Prevents asymmetric barrel thinning |
| Antipad clearance | Enough for the larger drill | Avoids shorting to the plane |
| Trace keep-out | Away from the backdrill edge | Prevents damage to adjacent traces |
| Post-drill fill | Required for via-in-pad or controlled depth | Prevents flux and moisture trapping |
The two numbers that decide the result are the target stub length and the depth tolerance. If the design asks for a stub shorter than the fabricator can hold, the yield drops or the quote rises. Define both on the drawing.
Reliability checks
Backdrilling removes copper, so it changes the barrel:
- The remaining barrel must still carry the current and survive thermal cycling.
- The annular ring at the target layer must not be thinned by registration error.
- The backdrilled hole must be clean and, if filled, fully cured.
- The dielectric around the removed barrel can be more susceptible to CAF if moisture is trapped.
A first article should include a cross-section at the backdrilled vias, with the stub length and remaining barrel measured, plus a thermal stress check if the board is safety-critical.
What to put on the drawing
- Which vias are backdrilled, by layer and by connector.
- Target stub length and acceptable maximum.
- Backdrill diameter and depth tolerance.
- Antipad and trace keep-out requirements.
- Fill or plug requirement after backdrilling.
- Inspection method and sampling.
FAQ
Can every via be backdrilled?
No. Vias close to traces, planes or the board edge may not have room for the larger drill. The fabricator should review the layout before quoting.
Does backdrilling remove the stub completely?
No. A short stub remains. The target is to push its resonance above the signal bandwidth.
Is backdrilling cheaper than blind vias?
Usually yes for a through-hole design, because it avoids sequential lamination. The trade-off is an extra drilling step and depth control.
Does backdrilling affect reliability?
It can, if the remaining barrel is too thin or the annular ring is damaged. A cross-section at first article and a controlled depth recipe keep the risk manageable.
What to send for a backdrill review
- Stackup with target layers and via types
- Data rate and signal bandwidth
- Backdrill requirement per via or per connector
- Depth tolerance and stub target
- Fill or plug requirement
- Acceptance class
Send your stackup for a backdrill review, or review our multilayer capability and HDI capability.
Reviewed by the Benchuang process engineering team.